by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

HT15PP/4X-200-M12 Alternative: Voxintech Background Suppression Photoelectric Sensors

Looking for a replacement or alternative for the HT15PP/4X-200-M12? This compact photoelectric sensor with background suppression is used on conveyors, packaging machines and assembly lines across India. Below you will find its key specifications, the closest Voxintech alternatives, a side-by-side comparison and the points to check before you swap.

Note: the HT15 series is made by Leuze (part number 50155525 for the HT15PP/4X-M12). It is sometimes searched for together with Datalogic sensors – if you have a Datalogic background-suppression sensor to replace, send us its code and we will match it in the same way.

HT15PP/4X-200-M12 – Key Specifications

ManufacturerLeuze (HT15 series)
TypeDiffuse photoelectric sensor with background suppression
Adjustment range50–1,000 mm (multiturn potentiometer)
Light sourceRed LED, 660 nm
OutputPNP, light switching, max. 100 mA
Supply voltage10–30 V DC
Response time1 ms (500 Hz)
Connection“-200-M12” = 200 mm cable with M12 4-pin plug
Housing / protectionPlastic, 15 × 42.7 × 30 mm, IP67

Source: manufacturer’s published datasheet.

Best HT15PP/4X-200-M12 Alternative for Short Range: VTPE/M300-PE
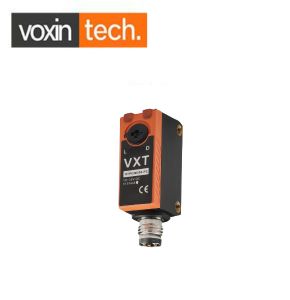
Voxintech VTPE/M300-PE background suppression photoelectric sensor – HT15PP/4X-200-M12 alternative

For most conveyor and packaging applications the object is well within 300 mm of the sensor. Here the Voxintech VTPE/M300-PE is the closest alternative: it uses the same working principle (background-suppression diffuse reflection), the same red 660 nm light and the same PNP output, with the same 1 ms response time and 500 Hz switching frequency.

  • Detection range 5–300 mm, switching distance set from 25–300 mm with a 6-turn potentiometer
  • Red light 660 nm, PNP open-collector output (≤100 mA)
  • 10–30 V DC supply, IP67
  • Compact 31 × 20 × 11 mm housing
  • M8 4-pin connector – use a matching M8 4-pin connector cable

Alternative for Longer Distances up to 1 m: VXT/TOF/2M-BP
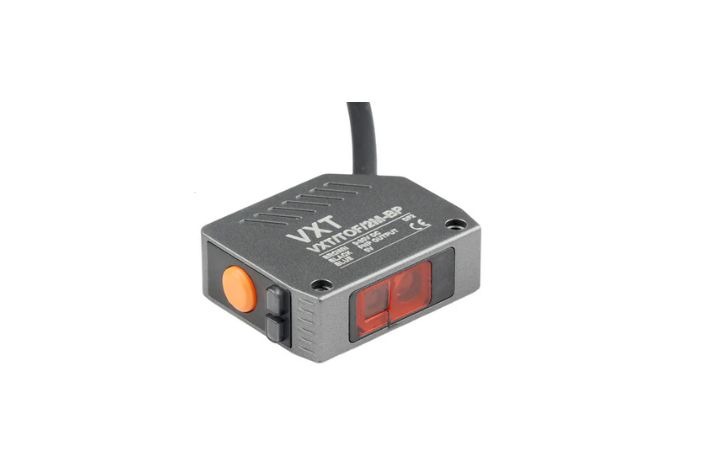
Voxintech VXT/TOF/2M-BP laser time-of-flight photoelectric sensor

If the sensor must detect objects between 300 mm and 1 m, choose the Voxintech VXT/TOF/2M-BP. It uses laser time-of-flight measurement, so the switching point stays stable on light and dark objects across its whole range.

  • Detection range 0.05–2 m, detects opaque objects from Ø5 mm
  • Laser diode 650 nm, Class 2
  • PNP open-collector output, NO/NC switchable, push-button setting
  • 9–30 V DC supply, 1 ms response time
  • 34.5 × 26.2 × 11 mm housing, 2 m cable, IP54

Side-by-Side Comparison

HT15PP/4X-200-M12VTPE/M300-PEVXT/TOF/2M-BP
PrincipleBackground suppressionBackground suppressionLaser time-of-flight
Range50–1,000 mm5–300 mm50–2,000 mm
LightRed LED 660 nmRed LED 660 nmLaser 650 nm, Class 2
OutputPNPPNPPNP, NO/NC switchable
Supply10–30 V DC10–30 V DC9–30 V DC
Response time1 ms1 ms1 ms
SettingPotentiometer6-turn potentiometerPush button
Connection200 mm cable + M12 4-pinM8 4-pin connector2 m cable
ProtectionIP67IP67IP54

Before You Replace – Checklist

  1. Measure the real detection distance. Up to 300 mm → VTPE/M300-PE. Up to 1 m → VXT/TOF/2M-BP.
  2. Check the mounting. The housing sizes are different, so you may need a new bracket or slotted holes.
  3. Check the connection. The original has an M12 plug on a short cable; VTPE/M300-PE needs an M8 4-pin cable, and VXT/TOF/2M-BP has a fixed cable for direct wiring.
  4. Check the wiring. On the original, pin 1 is +V, pin 3 is 0 V and pin 4 is the output. Confirm the pin-out on the Voxintech datasheet before connecting.
  5. Check the environment. For wash-down or wet areas, choose the IP67 VTPE/M300-PE.

HT15PP/4X-200-M12 Alternative – FAQs

Is VTPE/M300-PE a direct replacement for HT15PP/4X-200-M12?

Electrically and functionally it is very close – same principle, light colour, PNP output and response time – but its range is 300 mm instead of 1,000 mm, and it uses an M8 connector and a smaller housing. For distances above 300 mm, use VXT/TOF/2M-BP.

Do you supply these sensors from stock in India?

Voxintech supplies photoelectric sensors from Delhi NCR to customers across India. Contact us for current availability and price.

Can you match other Leuze, Datalogic, Sick or Omron sensor codes?

Yes. Send us the full model code and a short description of the application, and we will suggest the closest Voxintech alternative. See our full range of photoelectric sensors.

Need a price for the HT15PP/4X-200-M12 alternative? Call or WhatsApp +91 99530 39482, email info@voxintech.com, or request a quote with your detection distance and connection type.
by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

Ultrasonic Sensor Working Principle: Blind Zone, Calibration, Teach-In and PLC Wiring

Ultrasonic sensors measure distance with sound, which makes them excellent for liquids, transparent objects and dusty environments – but only if you understand how they work and where their limits are. This guide explains the ultrasonic sensor working principle, the blind zone, temperature effects, foam and vapour, how to calibrate a level sensor, teach-in and wiring to a PLC, and how ultrasonic compares with photoelectric and capacitive sensors.

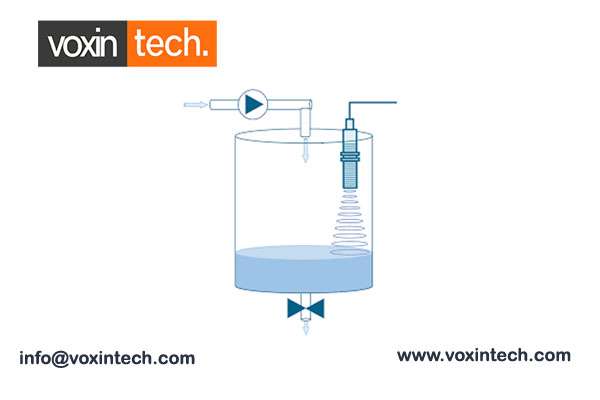
Ultrasonic sensor working principle – ultrasonic level sensor measuring liquid level in a tank

Ultrasonic Sensor Working Principle

An industrial ultrasonic sensor contains a transducer that works as both a loudspeaker and a microphone. It sends a short burst of high-frequency sound – far above human hearing – then switches to listening mode and waits for the echo from the target. The sensor’s electronics measure the time of flight, the time between sending the pulse and receiving the echo, and calculate the distance:

Distance = (speed of sound × time of flight) ÷ 2

The division by two is because the sound travels to the target and back. The calculated distance is then converted into a switching signal (PNP/NPN) or an analog signal (4–20 mA or 0–10 V) for the PLC. Because this ultrasonic sensor working principle relies on sound rather than light, the target’s colour, transparency and surface finish make little difference. Read more about the ultrasonic transducer.

Ultrasonic Sensor Blind Zone (Dead Band) Explained

Right after sending a pulse, the transducer is still “ringing” and cannot hear an echo. Any target inside this distance cannot be measured – this is the blind zone, also called the dead band. On industrial sensors it is shown as the first figure of the sensing range; for example, a 50–800 mm sensor has a 50 mm blind zone, and long-range sensors have larger blind zones.

In practice this means:

  • On a tank, mount the sensor so the highest liquid level stays below the blind zone – use a stand-off nozzle if needed.
  • On a machine, make sure the target can never come closer than the minimum range, or the output may become unpredictable.

Temperature Compensation

The speed of sound in air changes with temperature – by roughly 0.17 % per °C. Without correction, a reading taken at 45 °C on a hot summer tank roof would differ by several percent from the same reading at 15 °C. Most industrial sensors deal with this through temperature compensation: a built-in temperature sensor corrects the calculation automatically (check the datasheet for your model). To get the best accuracy:

  • Let the sensor warm up for a few minutes after power-on.
  • Shade it from direct sunlight where possible.
  • Avoid mounting it where hot air or steam flows across the sensor face.

Ultrasonic Sensor Foam and Vapour – Common Problems

  • Foam absorbs sound, so the echo may be weak or come from the top of the foam rather than the liquid. Use a stilling pipe or choose a different technology for heavy foam.
  • Vapour and steam change the speed of sound and can form condensation on the sensor face. Keep the sensor away from inlets, ventilate the tank roof and keep the face clean.
  • Turbulence and agitators create an uneven surface and false echoes – mount away from inlets and moving parts and use the sensor’s averaging or filter settings if available.
  • Obstructions such as ladders, pipes and tank walls can return a stronger echo than the liquid. Keep the sound cone clear.

Ultrasonic Sensor for Transparent Objects and Shiny Surfaces

This is where ultrasonic sensors beat optical sensors. Light passes through glass, PET and clear film, and reflects unpredictably from polished metal – but sound reflects from all of them.

  • Ultrasonic sensor for transparent objects – clear bottles, glass sheets, transparent film and labels. See our transparent label sensor.
  • Ultrasonic sensor for shiny surfaces – polished stainless steel, foil and chrome parts.

Keep the sensor face roughly perpendicular to flat, shiny targets; at a steep angle the echo may bounce away and be missed.

Ultrasonic Sensor vs Photoelectric Sensor

Ultrasonic sensorPhotoelectric sensor
Works onSound echoLight beam
Transparent and shiny targetsVery goodDifficult
Dust, mist, dirty lensesTolerantAffected
Speed and small objectsSlower, larger spotFaster, very small spot
Continuous distance outputCommon (4–20 mA / 0–10 V)Mainly on laser models

Choose ultrasonic for liquids, clear objects and dirty environments; choose a photoelectric sensor for fast counting and small parts.

Ultrasonic Sensor vs Capacitive Level Sensor

A capacitive level sensor detects the material by touching it or sensing it through a tank wall; it is usually a point-level switch (high or low level). An ultrasonic level sensor is non-contact and gives a continuous level reading from above. Choose ultrasonic for continuous level in water, diesel and most chemicals; choose capacitive for point-level alarms, sticky or foaming products, or small tanks where there is no space above the liquid.

How to Calibrate an Ultrasonic Level Sensor

  1. Measure the empty distance – from the sensor face to the tank bottom (or the lowest level you need). This becomes 4 mA (or 0 V).
  2. Measure the full distance – from the sensor face to the highest level. It must be greater than the blind zone. This becomes 20 mA (or 10 V).
  3. Set the two points on the sensor by teach-in, or scale them in the PLC.
  4. Convert distance to level in the PLC: level = empty distance − measured distance.
  5. Verify with a dipstick or known level at two points, then convert level to volume if the tank shape is known.

For mounting tips on tanks, see our ultrasonic water level sensor page.

Ultrasonic Sensor Teach-In Procedure

Many industrial ultrasonic sensors let you set switching points or the analog range without a laptop. The exact steps are in each datasheet, but a typical teach-in procedure is:

  1. Place the target at the first position (for example, the empty-tank level or the near switching point).
  2. Press the teach button – or connect the teach wire to +V or 0 V – for the time stated in the datasheet until the LED confirms.
  3. Move the target to the second position and repeat.
  4. Check the outputs at both points, then lock the settings if the sensor allows it.

Models without teach-in use a sensitivity potentiometer and configurable NO/NC outputs instead.

Ultrasonic Sensor Wiring to PLC

Voxintech industrial ultrasonic sensors run on 10–30 V DC and use an M12 connector, with outputs such as PNP + 4–20 mA, PNP + 0–10 V or 2 × NPN. A typical 4-wire connection is:

  • +V to the 24 V DC supply,
  • 0 V to supply 0 V and the PLC input common,
  • Switching output (PNP or NPN) to a digital input,
  • Analog output (4–20 mA or 0–10 V) to an analog input set to the matching mode.

Confirm pin numbers and wire colours from the sensor datasheet, use shielded cable for analog signals and keep it away from motor and VFD cables. Match PNP outputs to sourcing PLC inputs and NPN outputs to sinking inputs.

Frequently Asked Questions

What is the ultrasonic sensor working principle in one line?

The sensor sends a sound pulse, times how long the echo takes to return and converts that time into distance. Every other topic in this guide – blind zone, temperature and foam – follows from this ultrasonic sensor working principle.

Can ultrasonic sensors work in dusty environments?

Yes. Light dust has little effect on sound, which is why ultrasonic sensors are widely used for bins, silos and stone-crushing plants. Very heavy dust can weaken the echo at long range.

Why does my ultrasonic level sensor show a full tank when it is empty?

Usually the sensor is picking up an echo from a pipe, ladder or the tank wall, or the level has entered the blind zone. Re-position the sensor so the sound cone is clear.

Do ultrasonic sensors work in a vacuum?

No. Sound needs air or another gas to travel, so ultrasonic sensors cannot work in a vacuum.

Looking for prices and model selection? Read our ultrasonic sensor price in India guide or see the full range of industrial ultrasonic sensors. For application help, call or WhatsApp +91 99530 39482 or request a quote.

by Voxintech-admin@2022 Voxintech-admin@2022 1 Comment

Ultrasonic Sensor Price in India: 2026 Guide to Range, Output and Housing

Searching for ultrasonic sensor price in India usually turns up a confusing mix of hobby modules costing a few hundred rupees and industrial sensors that cost many times more. The difference is not just the brand – it is the range, output, housing and how long the sensor will survive on your plant. This guide explains what you are paying for and how to choose the right industrial ultrasonic sensor for level, distance and position sensing.

Voxintech industrial ultrasonic sensor M30 with M12 connector, IP67

What Decides Ultrasonic Sensor Price in India?

  • Sensing range – a 2 m sensor costs less than a 6 m or 8 m model, which needs a larger transducer and more power.
  • Output – simple NPN/PNP switching outputs cost less than analog 4–20 mA or 0–10 V outputs for continuous measurement.
  • Housing – PBT plastic, metal or AISI 316L stainless steel.
  • Size and thread – compact M18 sensors for short ranges, M30 sensors for long ranges.
  • Protection and temperature – IP67 sealing and an operating range of −20 °C to +70 °C for outdoor and plant use.
  • Support – datasheets, selection help, local stock and warranty.

For an exact quotation, share the distance you need to measure, the target (water, diesel, boxes, film), the output your PLC needs and where the sensor will be mounted.

Choosing the Range: 2 m, 4 m, 6 m or 10 m?

Pick a sensor whose maximum range is a little above your largest distance. Every ultrasonic sensor also has a blind zone close to its face where it cannot measure, so the target must stay further away than the minimum range. You can read more about how ultrasonic transducers measure distance.

You needChoose range groupTypical use
Up to about 0.8 m50–800 mmBottle and object detection, small tanks
About 2 m (ultrasonic sensor 2m range)900–2200 mmBin level, stack height, conveyor gaps
3–4 m (ultrasonic sensor 4m range)2200–3500 mm or 3500–6000 mmOverhead water tanks, sumps
About 6 m (ultrasonic sensor 6m range)3500–6000 mmLarge tanks, channels
Up to 8 m6000–8000 mmDeep tanks, rivers and dams

What about an ultrasonic sensor with 10 meter range? Voxintech’s industrial range goes up to 8 m. For deeper tanks or silos beyond that, a radar level transmitter is usually the better technology – ask us and we will advise honestly.

Output Options: 4–20 mA, 0–10 V, NPN/PNP or RS485

  • Ultrasonic sensor with 0–10 V output – continuous distance or level signal for controllers with a voltage input. Available as PNP + 0–10 V.
  • 4–20 mA output – the best choice for long cable runs and PLC analog inputs. Available as PNP + 4–20 mA.
  • Ultrasonic sensor with NPN PNP output – switching points for high/low level, pump on/off or object present. Available as 2 × NPN or PNP versions.
  • Ultrasonic sensor with RS485 – useful when many sensors share one network cable. Our standard range uses analog and switching outputs; if your system needs RS485/Modbus, tell us and we will suggest a suitable option or a converter.

All Voxintech industrial ultrasonic sensors run on 10–30 V DC and connect with an M12 plug.

Housing: Stainless Steel Body and IP67

An IP67 ultrasonic sensor is sealed against dust and temporary immersion, which is essential for tank tops, outdoor sumps and wash-down areas. Choose an ultrasonic sensor with stainless steel body (AISI 316L) for food, pharmaceutical and chemical plants, and PBT plastic or metal housings for general automation. See the full range on our industrial ultrasonic sensor page.

Ultrasonic Sensor M18 vs M30

The thread size tells you the body diameter and roughly the range:

  • M18 ultrasonic sensors – compact, for short ranges such as about 300 mm (cubic M18) and 900 mm (cylindrical M18). Ideal for machines and conveyors where space is tight.
  • M30 ultrasonic sensors – larger transducer for long ranges from 3.5 m up to 8 m, typically with PNP + 0–10 V or 4–20 mA output. Ideal for tank level and long-distance measurement.

Ultrasonic Level Sensor for Water, Diesel and Chemical Tanks

Water tanks

An ultrasonic level sensor for a water tank mounts on the tank roof, pointing straight down, and measures the distance to the water surface without touching it. Keep it away from the inlet pipe and the tank wall. See our ultrasonic water level sensor guide for mounting and output selection.

Diesel tanks

An ultrasonic level sensor for a diesel tank works well on day tanks and storage tanks for DG sets. Check whether the tank area is classified as a hazardous area – if it is, you must use equipment certified for that zone. More details are on our oil level monitoring page.

Chemical tanks

For an ultrasonic level sensor for a chemical tank, confirm that the housing material can withstand the vapours, and watch for foam, heavy condensation or vapour layers, which can absorb the ultrasonic pulse. A stainless steel version and a mounting nozzle that keeps the sensor face above the vapour usually help.

Level, Distance and Position Sensing

  • Ultrasonic sensor for level measurement – liquids, granules and powders in tanks, bins and silos.
  • Ultrasonic sensor for distance measurement – vehicle positioning, crane anti-collision and stack height.
  • Ultrasonic sensor for position sensing – roll diameter on winders and unwinders, and loop position on converting lines.

Ultrasonic Sensors on Conveyors and Packaging Lines

  • Ultrasonic sensor for conveyor – detects boxes, bags and products of any colour or surface, including shiny and transparent items that confuse optical sensors. See object detection using ultrasonic sensors.
  • Ultrasonic sensor for bottle detection – reliably detects clear glass and PET bottles on filling and labelling lines. See our food packaging page.
  • Ultrasonic sensor for web guiding – measures the edge or loop of film, paper and foil webs without contact. See roll diameter measurement.

Buying an Ultrasonic Sensor Online – What to Check Beyond Price in India

Before you buy an ultrasonic sensor online, make sure the listing tells you:

  • The sensing range and blind zone,
  • The output type and supply voltage,
  • The housing material, thread size and IP rating,
  • The operating temperature range,
  • Whether a datasheet, warranty and local technical support are available.

Hobby modules sold online are designed for prototypes and classrooms; they are not sealed or rated for continuous industrial use.

Looking for an ultrasonic sensor dealer near me? Voxintech supplies Italian-made industrial ultrasonic sensors, stocked and supported in India from Delhi NCR, with delivery across India.

Ultrasonic Sensor Price in India – FAQs

Why are industrial ultrasonic sensors more expensive than hobby modules?

Industrial sensors have sealed IP67 housings, industrial outputs such as 4–20 mA and 0–10 V, and robust transducers, and they are built for years of continuous use.

Can an ultrasonic sensor measure diesel or oil level?

Yes, in most cases. Check for hazardous-area requirements and avoid heavy foam or vapour.

What is the maximum range of your ultrasonic sensors?

Up to 8 m, depending on the model. For longer distances we can advise on alternative technologies.

Need a price? Call or WhatsApp +91 99530 39482, email info@voxintech.com, or request a quote with your range, target and output.

by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

Vibration Sensor Working Principle, PLC Wiring and Trip-Point Setting

An industrial vibration sensor looks like a simple stainless steel cylinder, but what happens inside it – and how you wire it, scale it and set its alarms – decides whether it protects your machine or just causes nuisance trips. This guide explains the vibration sensor working principle step by step, then covers wiring to a PLC, ISO 10816 limits, trip-point setting and how to stop false trips.

Industrial vibration sensor working principle and installation on a motor

Vibration Sensor Working Principle

Most industrial vibration sensors are built around a piezoelectric element – a small ceramic crystal clamped to a seismic mass inside the housing. When the machine vibrates, the mass pushes and pulls on the crystal, and the crystal produces an electrical charge that is proportional to the acceleration. That raw signal is then processed inside the sensor:

  1. Charge amplifier – converts the tiny charge from the crystal into a usable voltage.
  2. Filtering – removes frequencies outside the measuring band (for example 3 Hz to 1000 Hz on Voxintech VT series sensors).
  3. Integration – converts acceleration into vibration velocity in mm/s, the unit used for machine-health assessment.
  4. RMS detection – turns the alternating vibration signal into a steady overall value.
  5. 4–20 mA output stage – sends that value to the PLC as a standard current signal.

Because every step of the vibration sensor working principle happens inside the sensor, the PLC receives a clean, ready-to-use number. You can read more about the piezoelectric effect behind it.

mm/s vs g: Velocity vs Acceleration Measurement

The same vibration can be expressed in three ways – displacement (µm), velocity (mm/s) and acceleration (g). Which one you use depends on the frequency of the problem you want to catch:

MeasurementUnitBest forTypical use
DisplacementµmLow frequenciesShaft movement on large sleeve-bearing machines
Velocitymm/s RMSAbout 10–1000 HzOverall machine health: unbalance, misalignment, looseness
AccelerationgHigh frequenciesEarly bearing defects and gear mesh problems

For permanent monitoring and alarms on motors, pumps, fans and gearboxes, a velocity sensor in mm/s is usually the right choice, because it matches the severity limits in ISO standards and gives a stable reading. An acceleration sensor is the better choice when you want early warning of rolling-bearing damage on high-speed machines, usually with an analyser.

ISO 10816 Vibration Limits

ISO 10816-3 (now being replaced by ISO 20816-3) gives vibration severity zones for industrial machines above 15 kW, measured as velocity in mm/s RMS on the bearing housings:

Machine group and foundationA/B boundaryB/C boundaryC/D boundary
Group 2 (15–300 kW), rigid foundation1.42.84.5
Group 2 (15–300 kW), flexible foundation2.34.57.1
Group 1 (300 kW–50 MW), rigid foundation2.34.57.1
Group 1 (300 kW–50 MW), flexible foundation3.57.111.0

Zone A is a newly commissioned machine, zone B is acceptable for long-term running, zone C is acceptable only for a limited time, and zone D is severe enough to cause damage. Many plants use the B/C boundary as the warning level and the C/D boundary as the trip level – but always check the machine manufacturer’s recommendation first.

Vibration Sensor Wiring to PLC

2-wire vs 3-wire vibration sensor

A 2-wire (loop-powered) vibration sensor takes its power from the 4–20 mA loop itself, so only two wires run to the PLC. A 3-wire or 4-wire sensor has a separate supply (for example 10–30 V DC), a common 0 V and a 4–20 mA signal wire; the fourth wire can carry a second signal such as temperature. Voxintech VT series sensors use a separate 10–30 V DC supply and an M12 4-pin connector.

Wiring a 3/4-wire sensor to a PLC analog input

  • Connect sensor +V to the 24 V DC supply.
  • Connect sensor 0 V to the supply 0 V and to the analog input common.
  • Connect the 4–20 mA output to the analog input channel, set to “current” mode.
  • Use shielded cable and earth the shield at the panel end only.
  • Always confirm pin numbers from the sensor datasheet before connecting.

Scaling the signal

Vibration = (measured current − 4 mA) ÷ 16 mA × full-scale range. For example, on a sensor scaled 0–25 mm/s, a reading of 12 mA means (12 − 4) ÷ 16 × 25 = 12.5 mm/s. A reading below about 3.6 mA usually means a broken wire or a failed sensor – set a separate “sensor fault” alarm for it.

How to Set a Vibration Switch Trip Point

Whether you use a mechanical vibration switch or a 4–20 mA sensor with alarms in the PLC or a process indicator, the trip point should come from the machine itself:

  1. Record a baseline. Log the vibration at normal load for several days, including start-ups.
  2. Set the warning (alert) level at about 2 times the baseline, or at the ISO B/C boundary, whichever is lower.
  3. Set the trip (danger) level at about 4 times the baseline, or at the ISO C/D boundary.
  4. Add a time delay of a few seconds so short spikes do not stop the machine.
  5. Add a start-up bypass if the machine passes through a resonance while running up to speed.
  6. Review after one month and adjust if the levels are too close to normal running.

False Trip Vibration Switch Problems – Causes and Fixes

  • Trip point too close to normal level – raise it based on the recorded baseline.
  • No time delay – impacts, a passing forklift or a valve slam can trip the machine; add 3–10 seconds of delay.
  • Start-up and coast-down transients – use a start-up bypass timer.
  • Loose or poor mounting – a magnet, thin bracket or loose stud amplifies vibration; stud-mount directly on the bearing housing.
  • Electrical noise – route the cable away from VFD and motor power cables and earth the shield at one end only.
  • Structural resonance – if the reading changes sharply with small speed changes, move the sensor to a stiffer location.

Vibration Sensor Sensitivity Adjustment

Mechanical vibration switches have a sensitivity knob that changes the force needed to trip. A 4–20 mA vibration transmitter works differently: its measuring range is fixed at the factory, and you “adjust sensitivity” by changing the alarm set-points and time delays in the PLC or indicator. If your machine’s normal level uses only a small part of the range, choose a sensor with a lower full-scale range for better resolution.

Vibration Sensor Calibration

Industrial vibration sensors are calibrated by the manufacturer and normally need no adjustment on site. Good practice is to verify them every one to two years, or whenever readings look suspicious, using a portable vibration calibrator (a small shaker that applies a known vibration, commonly at 159.2 Hz). Compare the 4–20 mA output with the expected value; if it is outside tolerance, replace the sensor rather than trying to adjust it.

Frequently Asked Questions

What is the vibration sensor working principle in simple words?

A small mass inside the sensor presses on a piezoelectric crystal as the machine shakes. The crystal turns that movement into an electrical signal, and the built-in electronics convert it into a 4–20 mA value your PLC can read. Understanding this vibration sensor working principle also explains why stud mounting matters – any looseness changes what the mass feels.

Does a vibration sensor measure velocity or acceleration?

The sensing element measures acceleration. Velocity sensors integrate that signal internally and output mm/s, which is easier to compare with ISO limits.

What is a normal vibration level for a motor?

For a 15–300 kW motor on a rigid foundation, below about 2.8 mm/s RMS is generally acceptable for continuous running under ISO 10816-3. Trend your own machine for the best reference.

Why is my 4–20 mA vibration reading stuck at 4 mA?

Check the supply voltage, the wiring polarity and the PLC input mode. A steady 4 mA can also simply mean the machine is stopped or running very smoothly.

Looking for prices and model selection? Read our vibration sensor price in India buying guide or see the full range of industrial vibration sensors. For help with wiring or set-points, call or WhatsApp +91 99530 39482 or request a quote.

by Voxintech-admin@2022 Voxintech-admin@2022 1 Comment

Vibration Sensor Price in India: 2026 Buying Guide for 4–20 mA Sensors

If you are looking up vibration sensor price in India, you have probably found that most suppliers do not publish a price list. That is because the right sensor – and therefore the cost – depends on what you are monitoring, how the signal reaches your control system and where the sensor will be installed. This buying guide explains the options in plain language, so you can compare quotes properly and order the right sensor the first time.

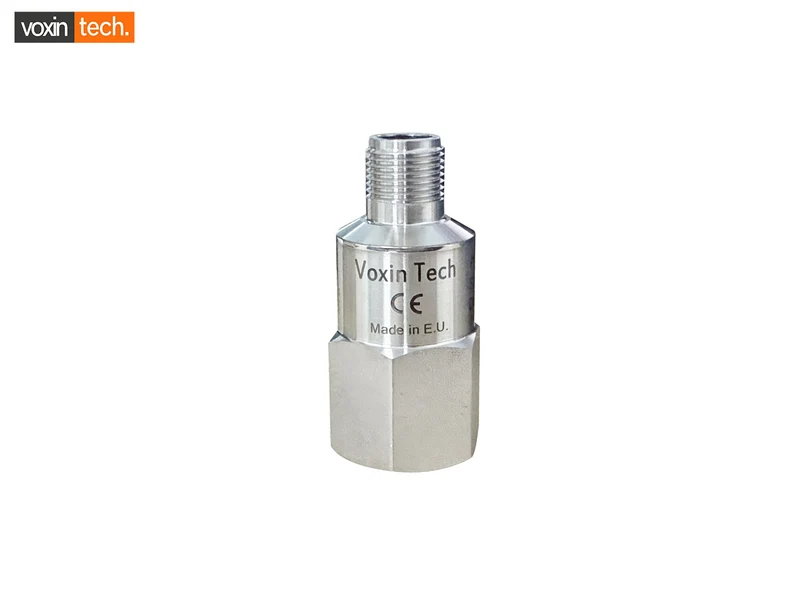
Voxintech VT series industrial vibration sensor with 4-20 mA output, stainless steel, CE

What Decides the Vibration Sensor Price in India?

Two sensors that look almost the same can be priced very differently. These are the factors that make the real difference:

  • Output type – a sensor with a 4–20 mA output that goes straight into a PLC costs more than a raw accelerometer, but saves you a separate signal conditioner or monitoring module.
  • Measured value – velocity (mm/s) sensors for machine health versus accelerometers for high-frequency analysis.
  • Temperature output – models with a second, bearing-temperature output add a little to the cost but replace a separate temperature probe.
  • Housing and protection – AISI 316L stainless steel and IP67 or IP69 ratings for washdown, outdoor and chemical areas.
  • Connector and cable – M12 connector versions with a matching cable versus fixed-cable models.
  • Quantity and support – project quantities, commissioning help and local stock all affect the final price.

The best way to get an accurate price is to share the machine type, speed, mounting point and the input on your PLC or panel. You will then receive a quote for a sensor that actually fits – rather than a cheap one that has to be replaced.

Vibration Sensor with 4–20 mA Output – Why Most Plants Choose It

A vibration sensor with 4–20 mA output (also called a vibration transmitter) converts the machine’s vibration into a standard current signal. That makes it the simplest vibration sensor for PLC and SCADA systems: wire it to any analog input, scale 4 mA as zero and 20 mA as full scale, and set your alarm limits in the PLC.

Voxintech VT series sensors, for example, measure vibration velocity from 0 to 100 mm/s over 3 Hz to 1000 Hz, give a 4–20 mA output, run on 10–30 V DC and connect through an M12 4-pin connector. Versions with an optional temperature output (10 mV/°C) are also available. See the full range on our industrial vibration sensor page.

Loop-powered vs separately powered 4–20 mA sensors

A loop-powered vibration sensor uses the same two wires for power and signal, which is convenient when you are replacing an existing 2-wire transmitter. A separately powered sensor has its own 10–30 V DC supply and returns the 4–20 mA signal on another wire, which allows extra functions such as a temperature output on the same connector. Before ordering, check whether your PLC analog card supplies loop power or expects an active (powered) signal – it is the most common wiring mistake on site. The Voxintech VT series uses a separate 10–30 V DC supply.

Velocity Sensor or Accelerometer?

A vibration velocity sensor reports vibration in mm/s, the unit used by machine vibration-severity standards such as ISO 10816 / ISO 20816. It responds best to the problems that matter on most plant machinery – unbalance, misalignment, looseness and general bearing wear – and the reading is easy to trend and alarm.

A vibration accelerometer sensor (see accelerometer) measures acceleration (g) and is more sensitive at high frequencies. It is preferred for early bearing-defect and gear-mesh analysis, usually together with a vibration analyser or online monitoring system.

Rule of thumb: for continuous protection and alarming on motors, pumps, fans and gearboxes, choose a velocity sensor with 4–20 mA output. For detailed diagnostics on high-speed or critical machines, add accelerometers and an analysis system.

Contact Type Vibration Sensor and Mounting

Industrial vibration sensors are contact type – they must be firmly attached to the machine so that the vibration passes into the sensor. How you mount it has a bigger effect on accuracy than most people expect:

  • Stud mounting is the best method. A vibration sensor mounting stud screws into a tapped hole on the bearing housing. Always check the thread on the datasheet – common sizes include M8 and 1/4″-28 UNF – and use an adaptor stud if your machine is tapped differently.
  • Adhesive or weld-on pads are used where drilling the casing is not allowed.
  • Magnetic bases are fine for temporary checks with a portable meter, but not recommended for permanent monitoring.

Do not confuse the mounting thread with the connector. On Voxintech sensors the electrical connection is a standard M12 4-pin connector – vibration sensor M8 / M12 thread searches often mix these two up. Mount the sensor on the bearing housing in the radial direction, as close to the bearing as possible, on a flat, clean, paint-free surface.

Choosing a Sensor by Machine

MachineWhere to mountWhat to watch for
Electric motorDrive-end bearing housing, radialBearing wear, unbalance, soft foot
Fan / blowerFan-side bearing, radialUnbalance from dust build-up, looseness
Cooling-tower fanGearbox or motor housingBlade unbalance, gearbox wear; choose IP67/IP69 for wet areas
GearboxInput and output bearing housingsBearing and gear wear
CompressorMain bearing housingsMisalignment, looseness, bearing faults
CrusherMain shaft bearing housingsShock loading, bearing damage; choose a rugged stainless steel sensor

Industry-specific advice is available for cement plants, mining and food and beverage.

Vibration Switch or Vibration Transmitter?

A traditional vibration switch for cooling towers or for motor protection is a simple trip device: when vibration passes a set level, a contact opens and the machine stops. It is cheap, but it gives no warning – you only find out when the machine has already tripped.

A 4–20 mA vibration transmitter does the same job and more. Connected to a PLC, or to a VT 406D process indicator in the panel, it shows the live vibration level and lets you set two limits – a warning alarm and a trip. Maintenance teams see the level rising over days or weeks and can plan a repair before the breakdown.

Building a Simple Vibration Monitoring System

A practical vibration monitoring system in India does not need expensive software. For most plants it is:

  1. A 4–20 mA vibration sensor on each critical machine,
  2. An M12 connector cable back to the panel,
  3. A PLC analog input or a process indicator with alarm outputs,
  4. Alarm limits set from the machine’s normal running level.

Start with the machines whose failure stops production, record their normal vibration for a week, then set your warning limit above that level.

Buying a Vibration Sensor Online in India – What to Check

If you plan to buy a vibration sensor online in India, look beyond the price:

  • Is the measuring range and unit (mm/s or g) stated clearly?
  • Is the output 4–20 mA, and is it loop-powered or separately powered?
  • Is a datasheet with mounting thread and connector pin-out available?
  • Is the country of origin and warranty stated?
  • Can the seller help with selection and commissioning, and supply spares later?

Looking for a vibration sensor dealer near me? Voxintech supplies French-made VT series vibration sensors, stocked and supported from Delhi NCR, with delivery to customers across India.

Vibration Sensor Price in India – FAQs

What is the price of a vibration sensor in India?

It depends on the output type, temperature option, housing and quantity. Share your machine details and PLC input type with us and you will receive an exact quotation.

Can I connect a vibration sensor directly to a PLC?

Yes. A vibration sensor with 4–20 mA output connects to a standard PLC analog input. Check whether the input expects a loop-powered or an active signal.

Which vibration sensor is best for motors?

For continuous monitoring and alarms, a velocity sensor with 4–20 mA output mounted on the drive-end bearing housing is the most practical choice.

Do I need a vibration switch or a transmitter for a cooling tower fan?

A switch only trips the fan. A transmitter with a 4–20 mA output shows the trend and gives an early warning, which helps you avoid unplanned stoppages.

Need a price or help choosing? Call or WhatsApp +91 99530 39482, email info@voxintech.com, or request a quote with your machine details.

by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

Rotary Encoder Supplier Across India: VXT Encoders for Every Industrial Hub

Key takeaways

  • VXT encoders are supplied across India, from Delhi NCR and Gujarat to Tamil Nadu and West Bengal.
  • The range covers 10 models from 360 to 5000 PPR in 38, 40, 50 and 58 mm sizes.
  • Each industry cluster has a typical choice, from textile length counting to CNC positioning.
  • Send us your current model number for a matching VXT recommendation.
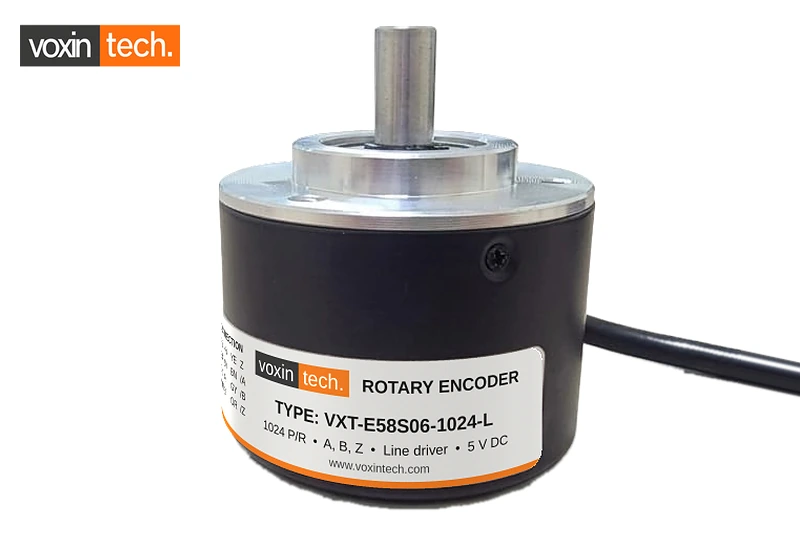
VXT-E58S06-1024-L Voxintech incremental rotary encoder
VXT-E58S06-1024-L Voxintech Rotary Encoder

India's manufacturing is spread across hundreds of industrial clusters, from packaging units in Gujarat to auto component plants in Tamil Nadu and textile mills in Punjab. Each one relies on rotary encoders for speed, length and position feedback. We supply the VXT incremental encoder range across India, with selection help, wiring support and a 1-year warranty, wherever your machine runs.

The VXT encoder range we supply

ModelSize / shaftPPROutputBest for
VXT-E38S06-0360-NPN38 mm / 6 mm360NPN open collectorCompact length and angle measurement
VXT-E40S06-0500-NPN40 mm / 6 mm500NPN open collectorSpeed monitoring, simple counting
VXT-E40S06-1024-NPN40 mm / 6 mm1024NPN open collectorGeneral PLC counting
VXT-E40S06-1024-PNP40 mm / 6 mm1024PNP open collectorPNP-input controllers
VXT-E40S06-1024-L40 mm / 6 mm1024Line driverServo and motion inputs
VXT-E50S08-1000-T50 mm / 8 mm1000Totem poleConveyors, cut-to-length
VXT-E50S08-1024-T50 mm / 8 mm1024Totem poleUniversal PLC input
VXT-E50S08-2500-T50 mm / 8 mm2500Totem polePrint registration
VXT-E58S06-1024-L58 mm / 6 mm1024Line driverMotion control
VXT-E58S10-5000-L58 mm / 10 mm5000Line driverHigh-resolution positioning

All models support up to 300 kHz response frequency, carry IP54 protection and include a 2 m shielded cable.

North India

Delhi NCR is one of India's densest automation markets. We supply encoders to panel builders and machine OEMs in Delhi (Okhla, Narela, Bawana, Mundka, Wazirpur), Noida, Greater Noida, Ghaziabad, Gurugram, Manesar, Faridabad and Sonipat.

In Haryana, Punjab and Himachal Pradesh, our encoders go into textile, bicycle, auto component and pharmaceutical machinery in Ludhiana, Jalandhar, Amritsar, Mohali, Chandigarh, Panchkula, Panipat, Karnal, Ambala, Yamunanagar, Rohtak, Bahadurgarh, Baddi and Parwanoo.

Across Uttar Pradesh and Uttarakhand we serve Kanpur, Lucknow, Agra, Aligarh, Meerut, Moradabad, Bareilly, Varanasi, Prayagraj, Gorakhpur, Haridwar, Rudrapur, Dehradun and Kashipur.

In Rajasthan and Jammu & Kashmir: Jaipur, Bhiwadi, Neemrana, Alwar, Jodhpur, Udaipur, Kota, Bhilwara, Ajmer, Jammu and Kathua.

West India

Gujarat is a powerhouse for packaging, plastics, pharmaceuticals, ceramics and machine tools. We supply Ahmedabad (Naroda, Vatva, Changodar, Sanand), Surat, Vadodara, Rajkot, Jamnagar, Morbi, Bhavnagar, Anand, Gandhinagar, Mehsana, Ankleshwar, Bharuch, Vapi, Valsad and Gandhidham, along with Daman and Silvassa.

Maharashtra has some of the country's largest automotive, engineering and printing clusters: Mumbai, Thane, Navi Mumbai, Bhiwandi, Vasai-Virar, Palghar, Pune (Chakan, Bhosari, Pimpri-Chinchwad, Ranjangaon, Talegaon), Nashik, Aurangabad (Waluj, Shendra), Nagpur (Butibori, Hingna), Kolhapur, Satara, Sangli, Ahmednagar, Jalgaon and Solapur.

In Goa: Verna, Margao and Panaji.

Central India

Madhya Pradesh and Chhattisgarh: Indore, Pithampur, Dewas, Bhopal, Mandideep, Gwalior, Jabalpur, Ujjain, Raipur, Bhilai, Durg and Bilaspur, serving steel, auto component, food processing and pharmaceutical plants.

South India

Tamil Nadu is a leading region for automotive, textiles and engineering: Chennai (Ambattur, Guindy, Sriperumbudur, Oragadam), Coimbatore, Tiruppur, Hosur, Madurai, Salem, Erode, Karur, Tiruchirappalli, Sivakasi and Tuticorin.

Karnataka: Bengaluru (Peenya, Bommasandra, Whitefield, Jigani, Doddaballapur), Mysuru, Hubballi-Dharwad, Belagavi, Mangaluru, Tumakuru and Davanagere.

Telangana and Andhra Pradesh: Hyderabad, Secunderabad, Medak, Patancheru, Visakhapatnam, Vijayawada, Guntur, Nellore, Tirupati, Sri City and Anantapur.

Kerala: Kochi, Thiruvananthapuram, Kozhikode, Thrissur and Palakkad.

East and North-East India

West Bengal, Odisha, Jharkhand and Bihar: Kolkata, Howrah, Durgapur, Asansol, Haldia, Kharagpur, Siliguri, Bhubaneswar, Cuttack, Rourkela, Jharsuguda, Angul, Jamshedpur, Ranchi, Bokaro, Dhanbad and Patna, serving steel, paper, cement and heavy engineering.

North-East: Guwahati and the wider region.

Which encoder do different industries buy?

IndustryCommon citiesTypical VXT choice
Packaging machineryAhmedabad, Vapi, Mumbai, Delhi NCR, Pune, BaddiVXT-E40S06-1024-NPN, VXT-E50S08-1024-T
Printing and convertingDelhi, Sivakasi, Mumbai, Ahmedabad, KolkataVXT-E50S08-2500-T, VXT-E38S06-0360-NPN
Textile machinerySurat, Tiruppur, Coimbatore, Ludhiana, Panipat, BhilwaraVXT-E38S06-0360-NPN, VXT-E50S08-1000-T
Automotive and auto componentsPune, Chennai, Manesar, Gurugram, Aurangabad, Pithampur, HosurVXT-E40S06-1024-PNP, VXT-E58S06-1024-L
CNC and machine toolsRajkot, Bengaluru, Coimbatore, Ludhiana, PuneVXT-E58S10-5000-L, VXT-E40S06-1024-L
Steel, wire and cut-to-lengthJamshedpur, Raipur, Bhilai, Rourkela, LudhianaVXT-E50S08-1000-T, VXT-E50S08-1024-T
Pharma and food processingBaddi, Hyderabad, Ahmedabad, Vadodara, Sikkim, IndoreVXT-E40S06-1024-NPN, VXT-E40S06-1024-PNP

Looking for an Autonics or Omron alternative near you?

Many customers in these cities come to us when they need a replacement for an Autonics or Omron encoder. Our cross-reference guide shows which VXT model matches common types such as Omron E6B2-CWZ6C and Autonics E50S8-1024-3-T-24. Send us the model you use and we will suggest the closest VXT encoder.

How ordering works

  • Share the model you need, or the model you want to replace.
  • We confirm the right VXT encoder, datasheet and wiring.
  • We dispatch to your city and stay available for installation and after-sales support.

Frequently Asked Questions

Do you supply rotary encoders outside Delhi NCR?

Yes. We supply VXT encoders to customers across India, including all major industrial cities and clusters listed above.

Can I get technical help choosing an encoder?

Yes. Tell us your application, controller and the encoder you use today, and we will recommend the right VXT model.

Do VXT encoders come with a warranty?

Yes, VXT encoders come with a 1-year warranty.

Can I buy a single encoder for a replacement?

Yes. We supply single units for maintenance as well as volume quantities for machine builders.

Contact us

Wherever your plant is, contact us for VXT encoder datasheets, pricing and availability.

Autonics and Omron are trademarks of their respective owners. They are mentioned for reference only; VXT is not affiliated with these companies.

by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

How to Wire a Rotary Encoder to a PLC: A Practical Guide

Key takeaways

  • VXT wire colours: red +V, black 0 V, green A, white B, yellow Z; line drivers add brown /A, grey /B, orange /Z.
  • Configure PLC inputs for NPN or PNP sensors to match the encoder output.
  • Never connect a 5 V line driver encoder to a 24 V PLC input.
  • Earth the shield at one end only and keep encoder cables away from VFD and motor cables.
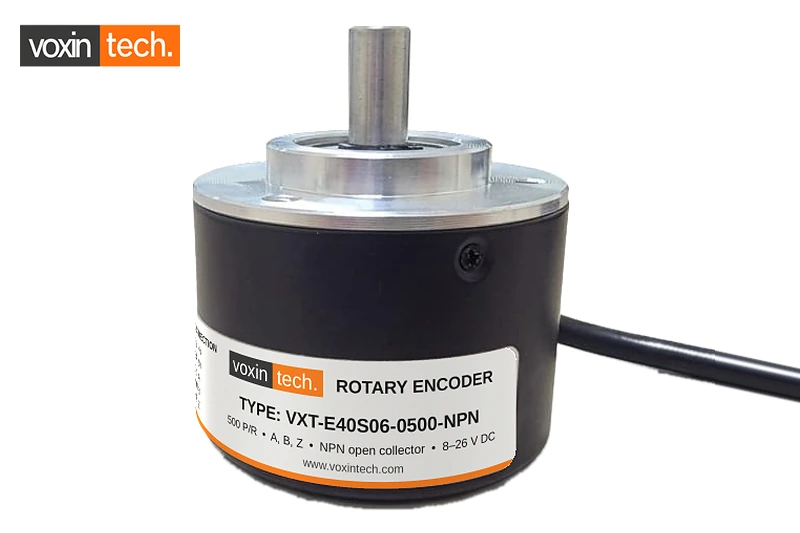
VXT-E40S06-0500-NPN Voxintech incremental rotary encoder
VXT-E40S06-0500-NPN Voxintech Rotary Encoder

Most encoder problems on commissioning day are wiring problems. The encoder is working, but the PLC counts nothing, counts in the wrong direction, or drifts at high speed. This guide covers the wiring for each VXT encoder output type, the standard wire colours, and the checks that fix most counting issues.

VXT encoder wire colours

All VXT encoders use the same colour code, which makes panel drawings and spares simpler.

Wire colourSignalUsed on
Red+V supplyAll models
Black0 VAll models
GreenAAll models
WhiteBAll models
YellowZ (index)Models with Z channel
Brown/ALine driver models
Grey/BLine driver models
Orange/ZLine driver models
Shield (bare)Frame groundAll models

Supply: 8 to 26 V DC for NPN, PNP and totem pole models; 5 V DC for line driver models. Always check the label before powering up.

Wiring an NPN open collector encoder

Models: VXT-E40S06-0500-NPN, VXT-E40S06-1024-NPN, VXT-E38S06-0360-NPN.

  • Red to +24 V, black to 0 V of the same supply that powers the PLC inputs.
  • Green (A), white (B) and yellow (Z, if present) to the PLC high-speed counter inputs.
  • Configure the inputs for NPN sensors. On many compact PLCs this means connecting the input common terminal (often marked S/S, COM or 1M) to +24 V. Check your PLC manual.
  • If the receiving device needs a voltage signal rather than a sinking input, add a pull-up resistor (typically 1 to 4.7 kΩ) from each output to +V.

Wiring a PNP open collector encoder

Model: VXT-E40S06-1024-PNP.

  • Red to +24 V, black to 0 V.
  • A, B and Z to the high-speed counter inputs.
  • Configure the inputs for PNP sensors. On many PLCs, this means connecting the input common to 0 V.
  • For a voltage-type receiver, add a pull-down resistor from each output to 0 V.

Wiring a totem pole encoder

Models: VXT-E50S08-1000-T, VXT-E50S08-1024-T, VXT-E50S08-2500-T.

Wire supply and signals the same way as above. The totem pole output drives the line both high and low, so it works whether the PLC inputs are configured for NPN or PNP sensors. No external resistor is needed in most installations.

Wiring a line driver encoder

Models: VXT-E40S06-1024-L, VXT-E58S06-1024-L, VXT-E58S10-5000-L.

  • Red to +5 V and black to 0 V, usually supplied by the drive or the line driver input module.
  • Connect each pair to a differential input: green (A) and brown (/A), white (B) and grey (/B), yellow (Z) and orange (/Z).
  • Use twisted-pair cable for any extension, keeping each signal with its inverted partner.
  • Do not connect a line driver encoder to a standard 24 V PLC input. It needs an RS-422 receiver, such as a line driver input card or a servo drive encoder input.

Connecting to popular PLCs

Compact PLCs widely used in India, such as Delta DVP, Mitsubishi FX and iQ-F, Siemens S7-1200, Omron CP series and others, include built-in high-speed counter inputs. The steps are similar on all of them:

  • Find which inputs support high-speed counting and which counter mode (single phase, up/down, or A/B phase) they offer.
  • Wire A and B to the inputs assigned to the A/B phase counter. Use Z only if you need a reference or reset.
  • Select the A/B phase (quadrature) mode and the multiplication (1x, 2x or 4x) in the PLC configuration.
  • Check the maximum input frequency for those inputs and compare it with your encoder frequency: rpm × PPR ÷ 60.

Shielding and noise: the most common cause of drifting counts

  • Earth the encoder cable shield at one end only, at the controller or panel earth bar.
  • Keep encoder cables at least 300 mm away from motor, VFD and servo power cables. Cross them at 90° if they must meet.
  • Do not run encoder signals in the same multi-core cable as AC control or power wiring.
  • For long runs or noisy panels, use a line driver encoder.
  • Fit ferrites or output filters on VFDs if counts jump when the drive starts.

Troubleshooting checklist

SymptomLikely causeFix
No counts at allWrong input type (NPN vs PNP), no supply, or input common wired wronglyCheck supply on red/black; check the input common; swap to the correct output type
Counts in the wrong directionA and B swapped, or direction settingSwap the A and B wires, or invert direction in the PLC
Counts drift or jumpNoise, shield not earthed, cable near VFDEarth the shield at one end; reroute the cable; consider a line driver encoder
Misses counts at high speedFrequency above input limitLower PPR, use a faster input, or use 1x decoding
Count is 4x too highPLC set to 4x quadratureAdjust scaling or select 1x mode
Encoder hot or damaged24 V applied to a 5 V line driverCheck the label; line driver models need 5 V DC

Frequently Asked Questions

What are the wire colours of a VXT encoder?

Red +V, black 0 V, green A, white B, yellow Z, and on line driver models brown /A, grey /B and orange /Z. The bare shield goes to frame ground.

Do I need a pull-up resistor for an NPN encoder?

Not when the PLC input is configured for NPN sensors. You need one only when the receiver expects a voltage signal.

Why is my encoder counting backwards?

Channels A and B are swapped relative to the direction your program expects. Swap the two wires or change the direction setting in the PLC.

Can I extend the encoder cable?

Yes, using shielded twisted-pair cable. For long runs or noisy environments, choose a line driver encoder such as VXT-E40S06-1024-L.

Need wiring help?

Send us your PLC model and the VXT encoder you are using, and we will help you with the connection. Contact us for datasheets, pricing and availability across India.

Delta, Mitsubishi, Siemens, Omron and Autonics are trademarks of their respective owners. They are mentioned for reference only; VXT is not affiliated with these companies.

by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

How to Choose Encoder PPR: Formula, Speed Limits and Worked Examples

Key takeaways

  • Distance per pulse = distance per revolution ÷ PPR.
  • Quadrature (4x) decoding gives four counts for every encoder pulse.
  • Output frequency = rpm × PPR ÷ 60; keep it below both the encoder and PLC input limits.
  • Choose the lowest PPR that meets your resolution; 1000 or 1024 PPR covers most machines.
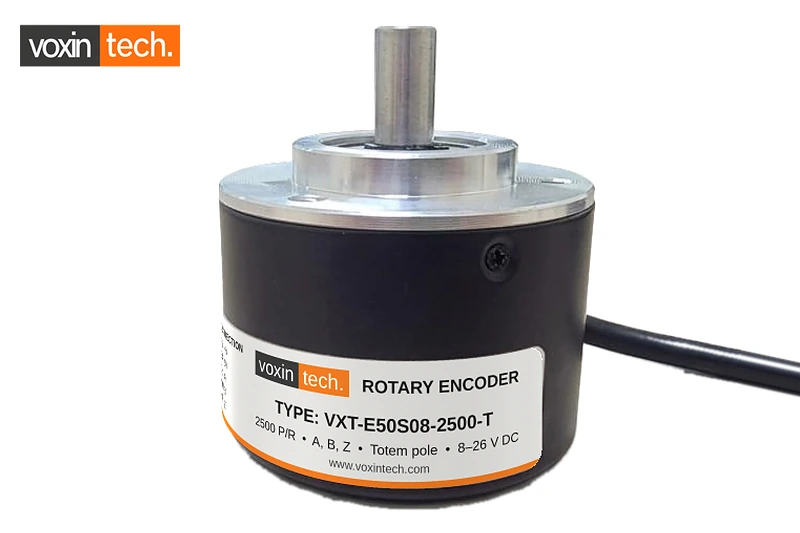
VXT-E50S08-2500-T Voxintech incremental rotary encoder
VXT-E50S08-2500-T Voxintech Rotary Encoder

PPR, or pulses per revolution, is the resolution of an incremental encoder. Pick it too low and your machine cannot position or measure accurately. Pick it too high and the pulse frequency at full speed may exceed what your PLC input or the encoder itself can handle. This guide gives you the formulas and worked examples to choose correctly, using the VXT range of 360, 500, 1000, 1024, 2500 and 5000 PPR.

The three numbers you need

  • Required resolution: the smallest movement you need to detect.
  • Maximum shaft speed in rpm.
  • Maximum input frequency of your PLC high-speed counter, counter module or drive.

Formula 1: Resolution per pulse

Linear distance per pulse = distance per revolution ÷ PPR

For a measuring wheel, the distance per revolution is the wheel circumference (π × diameter). For a ball screw, it is the screw lead.

Example: a 200 mm circumference measuring wheel with a VXT-E50S08-1000-T (1000 PPR) gives 200 ÷ 1000 = 0.2 mm per pulse.

Formula 2: Quadrature multiplies your resolution

An incremental encoder has two channels, A and B, 90° apart. A controller using quadrature decoding counts every rising and falling edge of both channels, which gives 4 counts per pulse:

  • 1024 PPR → 4096 counts per revolution.
  • 2500 PPR → 10,000 counts per revolution.
  • 5000 PPR → 20,000 counts per revolution.

Many PLC high-speed counters and all servo drives support 4x decoding. Check whether your counter is set to 1x, 2x or 4x mode, because it changes the scaling.

Formula 3: Pulse frequency at speed

Output frequency (Hz) = rpm × PPR ÷ 60

This frequency must stay below two limits:

  • the encoder's maximum response frequency (300 kHz for all VXT models), and
  • the maximum input frequency of your PLC or counter (often much lower; check the manual).

Maximum speed (rpm) = maximum frequency × 60 ÷ PPR

Maximum speed of each VXT encoder

VXT modelPPRElectrical limit at 300 kHzMechanical limitOperating limit
VXT-E38S06-0360-NPN36050,000 rpm6000 rpm6000 rpm
VXT-E40S06-0500-NPN50036,000 rpm6000 rpm6000 rpm
VXT-E50S08-1000-T100018,000 rpm6000 rpm6000 rpm
VXT-E40S06-1024 series, VXT-E50S08-1024-T, VXT-E58S06-1024-L102417,578 rpm6000 rpm6000 rpm
VXT-E50S08-2500-T25007200 rpm6000 rpm6000 rpm
VXT-E58S10-5000-L50003600 rpm6000 rpm3600 rpm

Your PLC input may set a lower limit. For example, if a counter input accepts up to 100 kHz, a 1024 PPR encoder is limited to about 5859 rpm on that input, and a 2500 PPR encoder to 2400 rpm.

Worked examples

Conveyor speed monitoring

A conveyor roller turns at up to 300 rpm and you only need speed. Resolution is not critical, so VXT-E40S06-0500-NPN (500 PPR) gives 2500 Hz at full speed, which any PLC counter can read.

Fabric or film length measurement

A 360 mm circumference measuring wheel on a VXT-E38S06-0360-NPN gives exactly 1 mm per pulse. At 120 m/min the wheel turns at about 333 rpm, producing 2000 Hz.

Packaging machine film feed

A feed roller with a 100 mm circumference needs 0.1 mm resolution. 100 ÷ 0.1 = 1000 PPR, so a VXT-E50S08-1000-T or VXT-E40S06-1024-NPN fits. With 4x decoding you get 0.025 mm per count, giving extra margin.

Print registration

A printing cylinder at up to 2000 rpm needs fine registration. A VXT-E50S08-2500-T gives 10,000 counts per revolution with 4x decoding and 83 kHz at 2000 rpm, within the input range of most high-speed counter modules.

Servo-driven rotary table

A rotary table driven at up to 600 rpm needs high angular resolution. A VXT-E58S10-5000-L gives 20,000 counts per revolution (0.018° per count) with 4x decoding and outputs 50 kHz at 600 rpm, using RS-422 signals for noise immunity.

Rules of thumb

  • Choose the lowest PPR that meets your resolution with some margin. It reduces frequency and makes the system more robust.
  • 1000 or 1024 PPR covers most packaging, conveyor and general automation work.
  • Use 360 PPR when you want one pulse per degree or simple length maths.
  • Use 2500 or 5000 PPR for registration and precision positioning, and check the speed limit.
  • When replacing an existing encoder, keep the same PPR unless you are ready to change the program scaling.

Frequently Asked Questions

What is the difference between PPR and CPR?

PPR is pulses per revolution on one channel. CPR (counts per revolution) is usually PPR × 4 when the controller uses quadrature decoding on channels A and B.

Is 1024 PPR better than 1000 PPR?

Neither is more accurate in practice. 1000 PPR makes decimal calculations easy; 1024 PPR is common in drives and existing programs. Match whatever your machine program expects.

Why does my encoder miss counts at high speed?

The pulse frequency is probably above the PLC input limit or the cable is too long for the output type. Lower the PPR, use a faster counter input, or switch to a line driver encoder.

What is the maximum speed of a 5000 PPR encoder?

For VXT-E58S10-5000-L, 3600 rpm, set by the 300 kHz response frequency.

Not sure which PPR fits your machine?

Tell us your speed, required resolution and controller model, and we will recommend the right VXT encoder. Contact us for datasheets, pricing and availability across India.

by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

Omron and Autonics Encoder Alternatives: VXT Cross-Reference Guide

Key takeaways

  • Decode your existing model number first: Omron suffixes and Autonics codes show the output type.
  • Match output type, then size, shaft, PPR and supply voltage.
  • Common matches: Omron E6B2-CWZ6C to VXT-E40S06 NPN; Autonics E50S8 T-type to VXT-E50S08.
  • Always compare the flange hole pattern before replacing on a running machine.
VXT-E40S06-1024-L Voxintech incremental rotary encoder
VXT-E40S06-1024-L Voxintech Rotary Encoder

When an encoder fails on a running machine, the first question is usually "what can replace it today?" Omron and Autonics encoders are among the most widely installed in India, so they are also the models we are asked to match most often. This guide shows how to read their model numbers, what to check before replacing, and which VXT encoder fits each common type.

Step 1: Decode the model number you have

Omron E6B2-C (40 mm)

The output type is in the suffix:

  • E6B2-CWZ6C: NPN open collector (published supply 5 to 24 V DC).
  • E6B2-CWZ5B: PNP open collector (12 to 24 V DC).
  • E6B2-CWZ3E: voltage output (NPN with pull-up).
  • E6B2-CWZ1X: line driver (RS-422 compatible, 5 V DC).

The resolution is printed after the model, for example "1000P/R", together with the cable length, for example "2M".

Omron 50 mm encoders

Omron's E6C2-C is a slim 50 mm encoder (for example E6C2-CWZ6C, NPN open collector), and the E6C3-C is a heavier-duty 50 mm series with an 8 mm shaft.

Autonics E40S, E50S and E58

Autonics model codes follow a clear pattern, for example E50S8-1024-3-T-24:

  • E50S8: series and size (50 mm housing, 8 mm shaft). E40S6 means 40 mm with a 6 mm shaft; E58SC10 means a 58 mm clamping-flange type with a 10 mm shaft.
  • 1024: pulses per revolution.
  • 3: output phases A, B, Z. 6 means A, /A, B, /B, Z, /Z (line driver).
  • T: output type. T = totem pole, N = NPN open collector, V = voltage output, L = line driver.
  • 24: supply 12 to 24 V DC. 5 means 5 V DC.

Step 2: The cross-reference table

Existing model (type)OutputMatching VXT model
Omron E6B2-CWZ6C 500P/RNPN open collectorVXT-E40S06-0500-NPN
Omron E6B2-CWZ6C 1024P/RNPN open collectorVXT-E40S06-1024-NPN
Omron E6B2-CWZ6C 360P/R (where space is tight)NPN open collectorVXT-E38S06-0360-NPN (38 mm, A/B only)
Omron E6B2-CWZ5B 1000P/RPNP open collectorVXT-E40S06-1024-PNP (update PLC scaling from 1000 to 1024)
Omron E6B2-CWZ1X 1024P/RLine driverVXT-E40S06-1024-L
Autonics E40S6-1024-3-N-24NPN open collectorVXT-E40S06-1024-NPN
Autonics E40S6-500-3-N-24NPN open collectorVXT-E40S06-0500-NPN
Autonics E40S6-1024-6-L-5Line driverVXT-E40S06-1024-L
Autonics E50S8-1000-3-T-24Totem poleVXT-E50S08-1000-T
Autonics E50S8-1024-3-T-24Totem poleVXT-E50S08-1024-T
Autonics E50S8-2500-3-T-24Totem poleVXT-E50S08-2500-T
58 mm line driver, 6 mm shaft, 1024 PPRLine driverVXT-E58S06-1024-L
58 mm line driver, 10 mm shaft, high resolutionLine driverVXT-E58S10-5000-L

Where your existing encoder uses a voltage output (Omron "3E" or Autonics "V"), a VXT totem pole model is usually the best substitute for 12 V and 24 V inputs, because it drives the line both high and low. Confirm with us if your receiver is a 5 V logic input.

Step 3: Check these five things before you swap

  • Mounting: compare the spigot diameter and the flange hole pattern. VXT-E40S06 and VXT-E38S06 use a ø20 mm spigot with 3 × M3 on a ø30 mm pitch circle. VXT-E50S08 uses a ø30 mm spigot with 3 × M4 on ø40 mm. VXT-E58 uses a ø36 mm spigot with 3 × M4 on ø48 mm.
  • Shaft diameter: 6, 8 or 10 mm. Your coupling bore must match.
  • Output type: NPN, PNP, totem pole or line driver must suit the input. This matters more than the brand.
  • PPR: match it, or update the scaling in the PLC or the electronic gear in the drive.
  • Supply voltage: 8 to 26 V DC for VXT NPN, PNP and totem pole models; 5 V DC for line driver models.

Other brands we are asked to match

Customers also bring us encoders from Hengstler, Kübler, Sick, Baumer, Koyo and Pepperl+Fuchs. The same five checks apply. Send us a photo of the label and the flange, and we will suggest the closest VXT model.

Why switch to VXT?

  • Equivalent outputs for the most common Omron and Autonics types.
  • Up to 300 kHz response frequency across the range.
  • Wide 8 to 26 V DC supply on open collector and totem pole models.
  • IP54 protection with a 2 m shielded cable.
  • Clear datasheets with wire colours, dimensions and timing.
  • Supply across India with selection and wiring support, and a 1-year warranty.

Frequently Asked Questions

What is the VXT equivalent of Omron E6B2-CWZ6C?

For 1024 PPR, the VXT-E40S06-1024-NPN; for 500 PPR, the VXT-E40S06-0500-NPN. Both are 40 mm encoders with a 6 mm shaft and NPN open collector output. Check the mounting hole pattern against your bracket.

What is the VXT equivalent of Autonics E50S8-1024-3-T-24?

The VXT-E50S08-1024-T: 50 mm housing, 8 mm shaft, 1024 PPR, totem pole output with A, B and Z channels.

Can I replace a line driver encoder with an NPN encoder?

Only if the receiver accepts single-ended NPN signals. Servo drives and RS-422 inputs need a line driver encoder such as VXT-E40S06-1024-L or VXT-E58S10-5000-L.

What if my PPR is not listed?

Contact us with your required PPR, size and output. We will advise the closest available VXT model or the scaling change needed.

Get a matching VXT encoder

Send us the model number or a label photo of your current encoder. Contact us for a cross-reference, datasheet, pricing and availability anywhere in India.

Omron, Autonics, Hengstler, Kübler, Sick, Baumer, Koyo and Pepperl+Fuchs are trademarks of their respective owners. They are mentioned for cross-reference only; VXT is not affiliated with, endorsed by or sponsored by these companies. Always verify dimensions and specifications against your application before replacing.

by Voxintech-admin@2022 Voxintech-admin@2022 No Comments

NPN vs PNP vs Totem Pole vs Line Driver: Which Encoder Output Do You Need?

Key takeaways

  • NPN outputs sink current; use them with PLC inputs configured for NPN sensors.
  • PNP outputs source current; use them with inputs configured for PNP sensors.
  • Totem pole outputs work with both; line drivers need an RS-422 differential receiver.
  • When unsure on a 24 V PLC, a totem pole encoder such as VXT-E50S08-1024-T is the safest choice.
VXT-E40S06-1024-PNP Voxintech incremental rotary encoder
VXT-E40S06-1024-PNP Voxintech Rotary Encoder

Two encoders can look identical, share the same size and PPR, and still refuse to work with your PLC. The difference is the output circuit. Getting it right is the single most important step when ordering an incremental encoder. This guide explains the four common output types in plain terms and shows the matching VXT encoder for each.

The short answer

Your controller inputChoose this outputVXT example
PLC input configured for NPN sensors (most common in India)NPN open collectorVXT-E40S06-1024-NPN
PLC input configured for PNP sensorsPNP open collectorVXT-E40S06-1024-PNP
Not sure, or mixed customer baseTotem pole (push-pull)VXT-E50S08-1024-T
Servo drive, motion controller, CNC, long cableLine driver (RS-422)VXT-E40S06-1024-L, VXT-E58S10-5000-L

NPN open collector

An NPN output switches the signal line to 0 V when active. It sinks current. The input on the other side must provide the current, either through its own internal circuit (inputs configured for NPN sensors) or through a pull-up resistor to +V.

  • Pros: the most widely used encoder output in Indian panels; works on any supply from 8 to 26 V DC on VXT models; simple and robust.
  • Watch out for: without a pull-up, you will not see a voltage on a multimeter, which confuses many first-time installers. Rise time depends on the pull-up resistor and cable length, so keep cables reasonably short at high pulse rates.
  • VXT models: VXT-E40S06-0500-NPN, VXT-E40S06-1024-NPN, VXT-E38S06-0360-NPN.

PNP open collector

A PNP output switches the signal line to +V when active. It sources current into the input. It suits PLC inputs configured for PNP sensors, which are common in European-designed machines and some OEM panels.

  • Pros: direct connection to PNP-type inputs; signal is "high" when active, which is intuitive to test.
  • Watch out for: a voltage-type receiver may need a pull-down resistor to 0 V.
  • VXT model: VXT-E40S06-1024-PNP.

Totem pole (push-pull)

A totem pole output has two transistors stacked between +V and 0 V. It actively drives the line high and actively drives it low. That gives sharp edges in both directions and means the output works with both NPN-type and PNP-type inputs.

  • Pros: universal compatibility with 12 V and 24 V PLC inputs; cleaner edges than open collector at higher frequencies; no external resistor in most cases.
  • Watch out for: never connect two totem pole outputs together, and do not connect the output directly to +V or 0 V.
  • VXT models: VXT-E50S08-1000-T, VXT-E50S08-1024-T, VXT-E50S08-2500-T.

In model codes from other makers you may see a similar output under different names. For example, Autonics uses the letter "T" for totem pole in codes such as E50S8-1024-3-T-24, "N" for NPN open collector and "L" for line driver.

Line driver (RS-422 differential)

A line driver outputs each channel twice: the signal and its inverted copy (A and /A, B and /B, Z and /Z). The receiver measures the difference between the pair, so noise picked up on the cable cancels out.

  • Pros: the best noise immunity; supports long cables; standard input on servo drives, motion controllers and CNC; allows broken-wire detection on many drives.
  • Watch out for: needs a differential (RS-422) receiver. It cannot be wired straight into a standard 24 V PLC input. VXT line driver models run on 5 V DC.
  • VXT models: VXT-E40S06-1024-L (40 mm), VXT-E58S06-1024-L (58 mm, 6 mm shaft), VXT-E58S10-5000-L (58 mm, 10 mm shaft, 5000 PPR).

Omron uses the suffix "1X" for line driver models in the E6B2-C series (E6B2-CWZ1X), while its NPN open collector version is E6B2-CWZ6C and its PNP version is E6B2-CWZ5B. If you are replacing one of these, match the output type first, then the size and PPR.

How to check what your PLC needs

  • Look at the high-speed counter section of the PLC manual. It will state whether the inputs are sink or source type, the input voltage, and the maximum input frequency.
  • Check how the input common (COM or S/S terminal) is wired. On many PLCs, wiring the common to +24 V configures the inputs for NPN sensors, and wiring it to 0 V configures them for PNP sensors.
  • For servo drives, check the encoder input specification. "Line driver" or "RS-422" means you need a differential encoder.
  • If in doubt, choose a totem pole encoder for 24 V PLC inputs.

Common mistakes we see

  • Ordering a line driver encoder for a 24 V PLC input. It will not count reliably and can be damaged by 24 V.
  • Connecting an NPN encoder to an input configured for PNP sensors. The input never turns on.
  • Powering a 5 V line driver encoder from 24 V. Always check the supply rating on the label.
  • Leaving the cable shield unconnected, or earthing it at both ends near a VFD.

Frequently Asked Questions

Is NPN or PNP better for an encoder?

Neither is better; they suit different inputs. NPN is more common in Indian panels and with Japanese and Taiwanese PLC brands. PNP is common in European-designed machines. Match the encoder to the input.

Can a totem pole encoder replace an NPN encoder?

In most 12 V and 24 V PLC applications, yes. A totem pole output drives the line both high and low, so it works with inputs configured for NPN or PNP sensors.

Why does my line driver encoder not work with my PLC?

Most standard PLC inputs are single-ended 24 V inputs. A line driver encoder outputs 5 V differential signals and needs an RS-422 receiver, such as a line driver input module or servo drive input.

Which VXT encoder should I stock as a universal spare?

For 24 V PLC applications, the VXT-E50S08-1024-T totem pole encoder covers both NPN-type and PNP-type inputs.

Need help choosing?

Send us your PLC or drive model and we will confirm the right VXT encoder output. Contact us for datasheets, pricing and availability across India.

Omron and Autonics are trademarks of their respective owners. They are mentioned for reference only; VXT is not affiliated with these companies.